R&D Capability
To continuously improve product quality stability and technical service capabilities, Liaoyang Zhongshi Chemical has jointly established a research and development platform with its upstream partner factories. This platform provides a comprehensive system for product development, analysis and testing, and application evaluation, enabling the company to offer customers more reliable chemical raw material solutions.
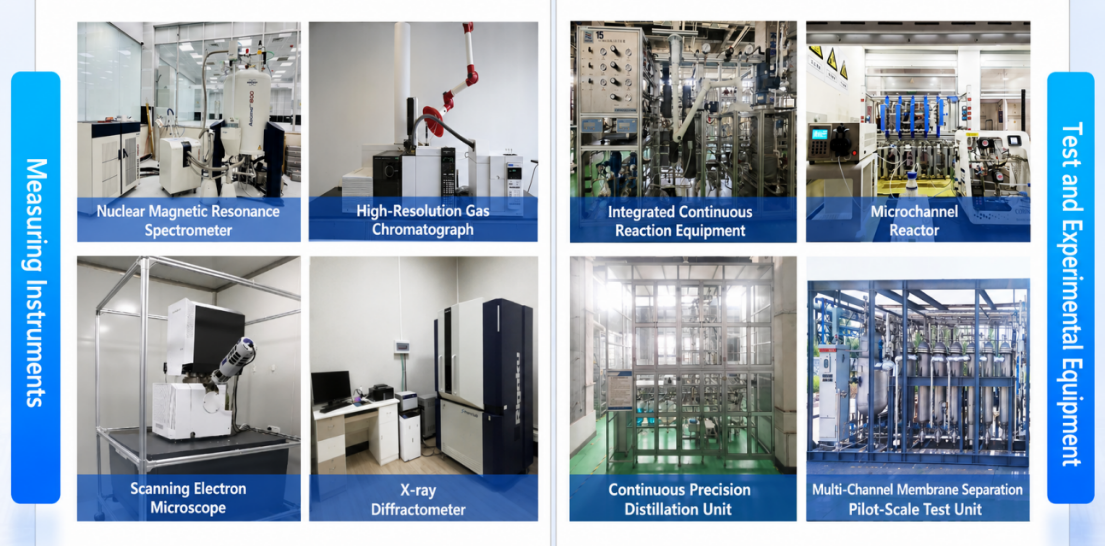
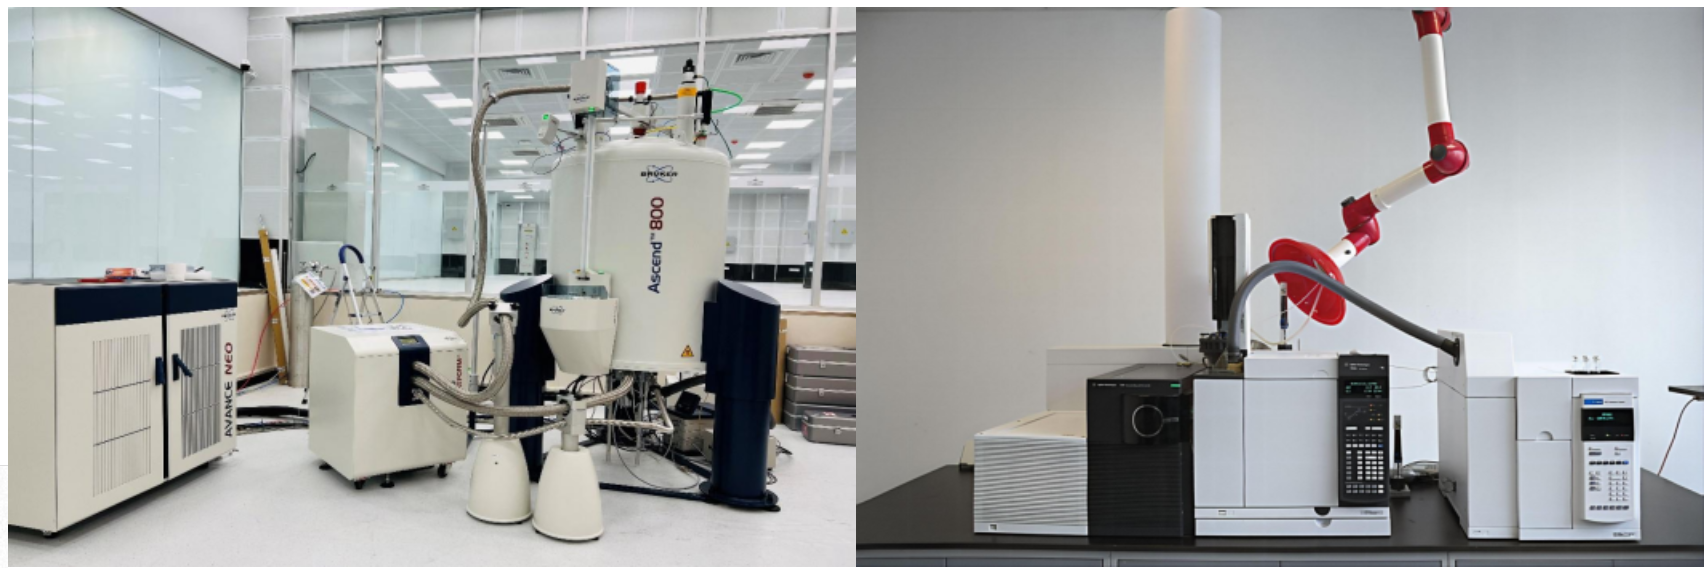
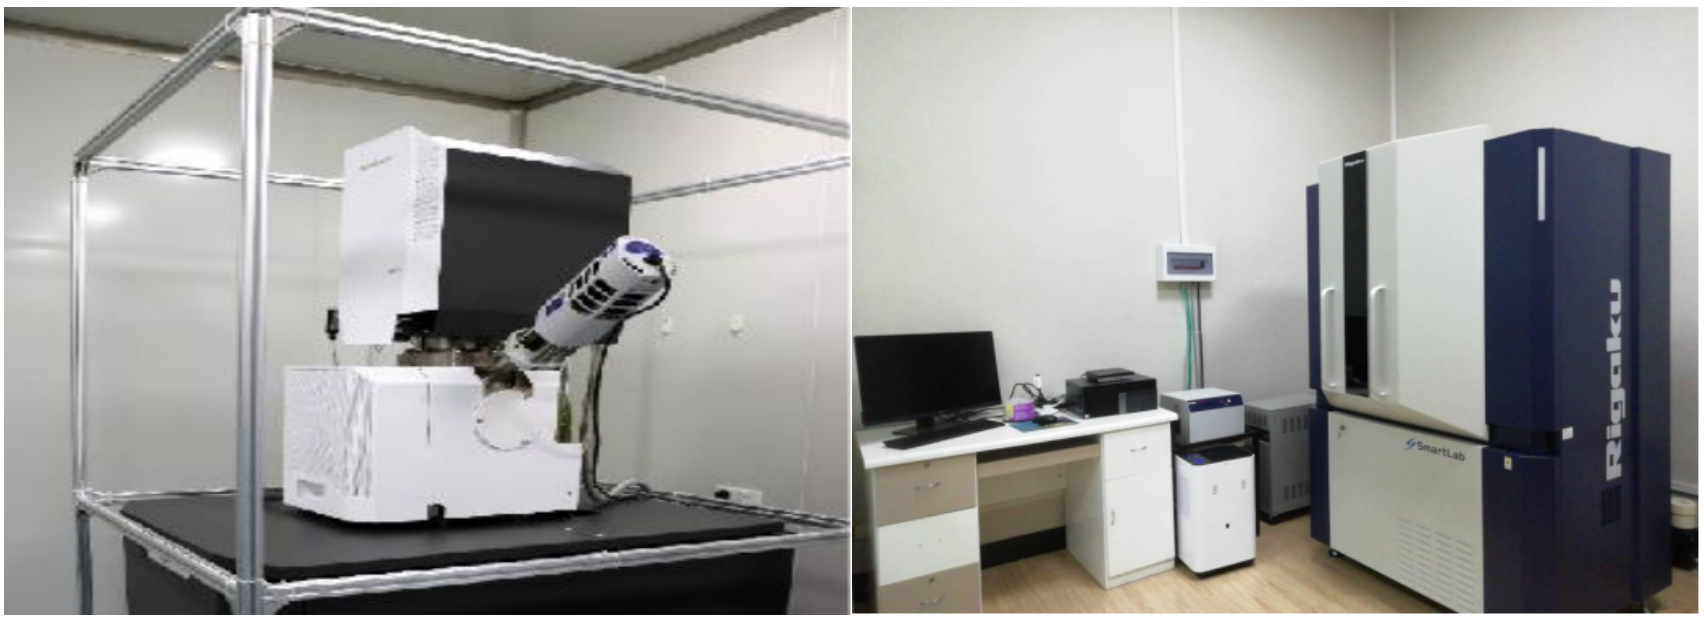
Currently, the R&D center possesses over 30 internationally advanced analytical and testing devices, including nuclear magnetic resonance (NMR), scanning electron microscopy (SEM), gas chromatography-mass spectrometry (GC-MS), SmartLab X-ray diffraction (XRD), and supercritical carbon dioxide extraction equipment. This allows for systematic testing and research on the composition, structure, purity, impurities, and application performance of chemical raw materials.
Simultaneously, the laboratory is accredited by the China National Accreditation Service for Conformity Assessment (CNAS) and has established a standardized quality management system and standardized testing procedures. This provides professional technical support for product quality control, process optimization, and customer application development.
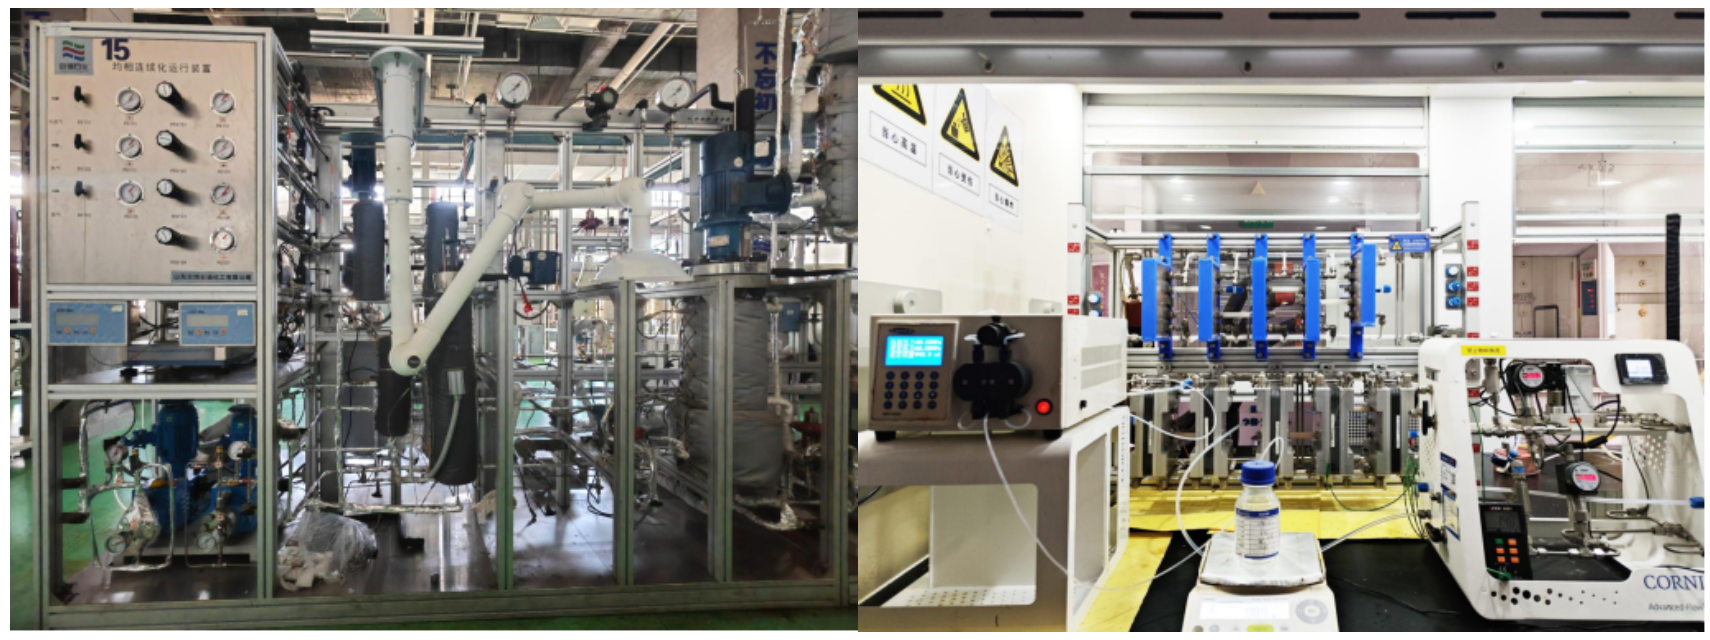
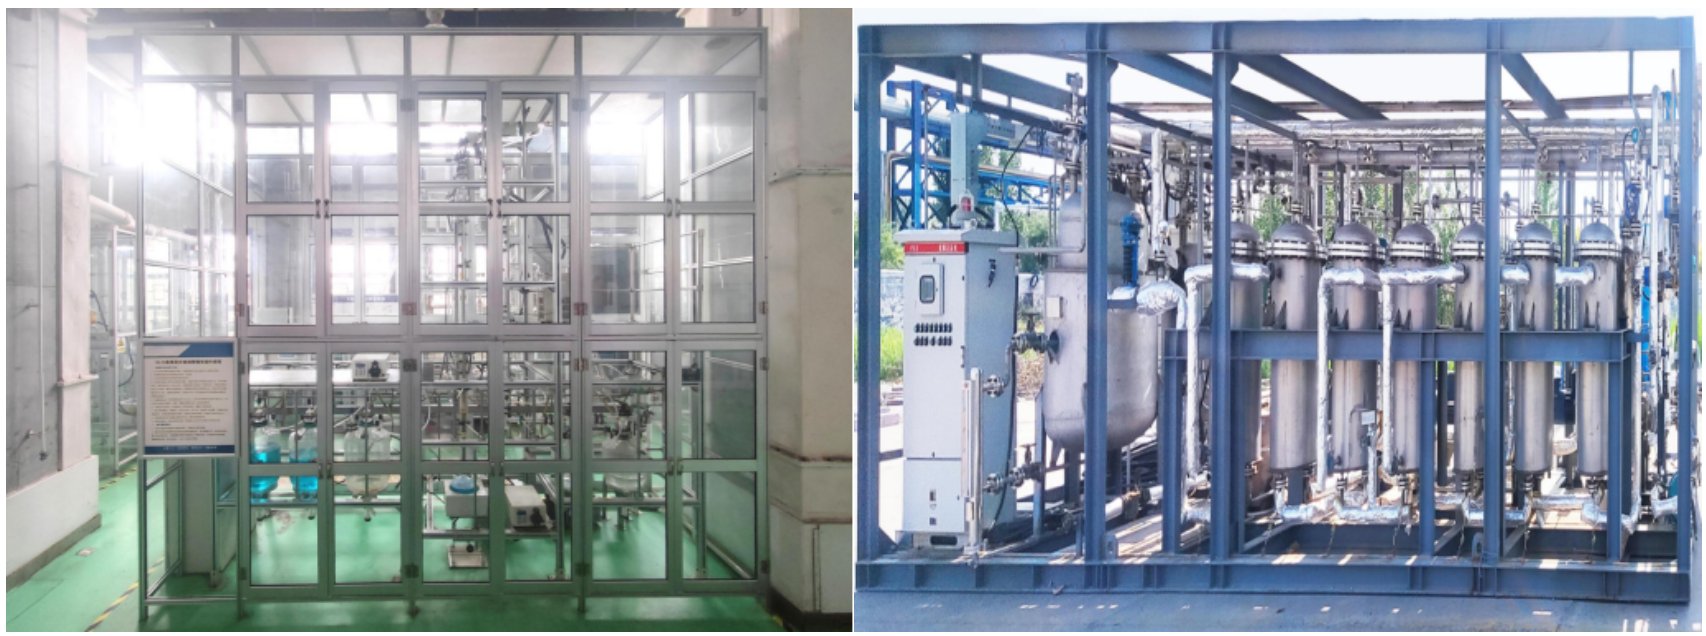
In terms of pilot-scale testing and process validation, the company is equipped with over 300 sets of experimental equipment, including catalyst evaluation devices and distillation testing systems. This enables research on solvent separation and purification, catalytic reaction evaluation, process scale-up validation, and new product development, providing a solid guarantee for product performance improvement and meeting customized customer needs. Furthermore, through its digital instrument sharing platform, the company can collaboratively reserve over 3,000 scientific research instruments and equipment from domestic universities and research institutions, further expanding its analytical testing capabilities and R&D depth. Relying on a collaborative innovation system integrating industry, academia, and research, the company can quickly respond to market demands, providing more professional product support and technical services to customers in the fields of plant extraction, pharmaceutical intermediates, pesticide manufacturing, electronic chemicals, and fine chemicals.
Core Technology Resources
·30+ sets of high-end analytical testing equipment
·300+ sets of process R&D and pilot-scale experimental devices
·CNAS accredited laboratory
·3,000+ shared scientific research instruments
·Covering the entire process of testing, analysis, R&D, and application evaluation
·Supporting product quality traceability and technology optimization services
Based on its advanced experimental platform and continuous innovation capabilities, the company continuously promotes the R&D and application of green chemicals, high-purity solvents, and fine chemical products, providing customers with more stable, safe, and high-quality product assurance.